Machine Learning Optimizes Strength and Ductility in ER5356 Aluminum WAAM
- Published
- Author
- Aura Moreno
- Reads
- 371
A model predicts four mechanical properties of circular-path ER5356 deposits; one confirmation build closely matched its predictions.
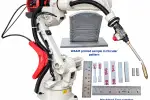
A machine learning model that predicts tensile strength, elongation, flexural strength and hardness from wire arc additive manufacturing (WAAM) settings could help engineers screen aluminum builds with fewer physical trials. In a study of ER5356 alloy deposited on a circular path, the model’s recommended settings produced a confirmation part whose measured properties were within 1.18% to 4.61% of predicted values.

That result is promising, with a key limitation: the validation came from a single build. The work, published in Scientific Reports, demonstrates a way to link process settings to several mechanical responses at once, but it doesn’t yet establish repeatability or performance outside the tested range.
Thirty builds map the process window
Researchers from King Faisal University in Saudi Arabia, Dr. Mahalingam College of Engineering and Technology, and Symbiosis Institute of Technology in India deposited ER5356 aluminum using a Fronius iWave 500i AC/DC welding unit and an ABB IRB 1520ID robotic arm. The system ran in cold metal transfer (CMT) mode, a wire arc process that can reduce heat input, spatter and droplet instability.
Every wall followed the same circular toolpath. The experiments therefore examine how four process settings affect properties within that path, rather than comparing different deposition strategies. The team varied wire feed speed from 7.5 to 9.5 m/min, travel speed from 6 to 10 mm/s, interpass temperature from 80 to 160°C, and shielding gas flow from 12 to 18 L/min.
A Taguchi L27 design, supplemented by three center-point runs, yielded 30 builds. Each was assessed for tensile strength, elongation, three-point bending and Vickers hardness. Across the experiments, tensile strength ranged from 243.60 to 289.70 MPa, while elongation ranged from 22.83 to 35.72%.
The center-point combination gave the strongest overall results in the initial set: 8.5 m/min wire feed, 8 mm/s travel, 120°C interpass temperature and 15 L/min shielding gas flow. Its top run measured 289.70 MPa tensile strength, 35.72% elongation, 391.21 MPa flexural strength and 70.72 HV hardness. The three center-point builds differed in tensile strength by less than 1.5 MPa, indicating close agreement across those repeats under the reported conditions.
One model predicts four properties
The researchers developed a stacked machine learning model called PG-MOSR. Alongside the four raw process settings, it uses derived descriptors intended to represent deposition intensity, heat buildup, cooling severity and shielding adequacy. This gives the model inputs framed in terms of process behavior, while keeping the measured outputs tied to mechanical tests.
In five-fold cross-validation, PG-MOSR achieved R² values of 0.7799 for tensile strength, 0.8299 for elongation, 0.8142 for flexural strength and 0.8599 for hardness. Against an XGBoost benchmark, it performed comparably for tensile strength and better on the other three properties; the benchmark’s hardness R² fell to 0.573.
Feature rankings pointed to wire feed speed as the strongest contributor to tensile and flexural predictions, while interpass temperature contributed most to elongation. The authors caution that these rankings describe statistical association in the dataset. They do not establish that a setting directly causes a particular property change, since process variables and the resulting deposit structure can interact.
There’s also a practical wrinkle in the physics-guided approach: a model trained only on the four raw settings performed better for all four outputs, with R² values between 0.8779 and 0.8885. The derived descriptors may help explain what the model is tracking, but in this dataset they didn’t improve predictive accuracy. That distinction matters when deciding whether interpretability features are useful for process decisions or mainly for analysis.

Optimization improved elongation in the confirmation build
After evaluating 50,000 parameter combinations, the optimizer selected settings predicted to deliver 295.20 MPa tensile strength, 40.10% elongation, 397.80 MPa flexural strength and 71.80 HV. The predicted tensile strength and elongation both exceeded the best values in the original 30-build set.
The confirmation build measured 288.90 MPa, 38.25% elongation, 385.60 MPa flexural strength and 70.95 HV. Those results fell between 1.18% and 4.61% from the model’s predictions. The predicted strength increase wasn’t realized: measured tensile strength came in below the original best run. Elongation, by contrast, reached 2.53 percentage points above the previous best.
Fracture surfaces showed ductile failure and clustered pores. The researchers suggest that porosity may help explain why tensile and flexural results were slightly below predictions. A single optimized build can check whether a model’s recommendation is plausible, but it can’t show how reliably the same settings will perform across repeated builds.
Useful scope, with clear limits
The model was developed for circular-path CMT deposition of ER5356 aluminum within the parameter ranges studied. Applying it beyond those ranges, or to a different alloy, deposition setup or toolpath, would require further validation. The optimization also left fatigue, corrosion, residual stress and porosity outside its measured objectives.
Those omissions define the next engineering questions. Computed tomography could provide more direct porosity measurements; in-situ thermal monitoring could add information about heat cycles; and a larger dataset could test whether the observed property relationships hold across more builds. For qualification work, the immediate need is repeat testing of the recommended settings and broader characterization of the deposited material.
Earlier WAAM machine learning studies have often focused on bead geometry, surface roughness or one mechanical response. Predicting four properties together gives process teams a wider view of the strength, ductility and hardness trade-offs, but the dataset here remains modest. Other metal additive manufacturing efforts illustrate different validation paths: a KAIST and POSTECH active learning framework for laser powder bed fusion Ti-6Al-4V used repeated print, test and retraining rounds, while a POSTECH and Korea Institute of Materials Science model for LPBF Al-Si-Mg incorporated process, microstructure and void data.
The WAAM study’s main contribution is a compact, multi-property model tied to measured builds, plus an optimization result that improved elongation in its confirmation part. For manufacturing use, the next step is to see whether repeated builds preserve that gain and whether the predictions remain useful when porosity and other service-relevant properties enter the picture.
The study, “Interpretable physics-guided multi-output learning for optimizing circular-path cold metal transfer wire arc additive manufacturing of ER5356 aluminium alloy,” was conducted by Syed Quadir Moinuddin, Gideon Ganesh Murugan, Hariharasakthisudhan Ponnarengan, Vishwanath Nagallapati, Mohammad Faseeulla Khan and Muhammad Iftikhar Faraz. The paper is available through Scientific Reports.


